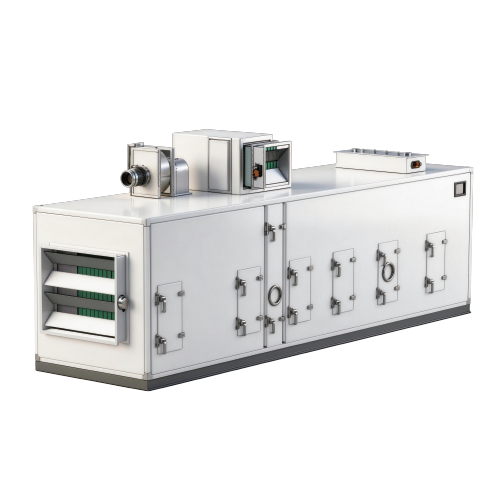
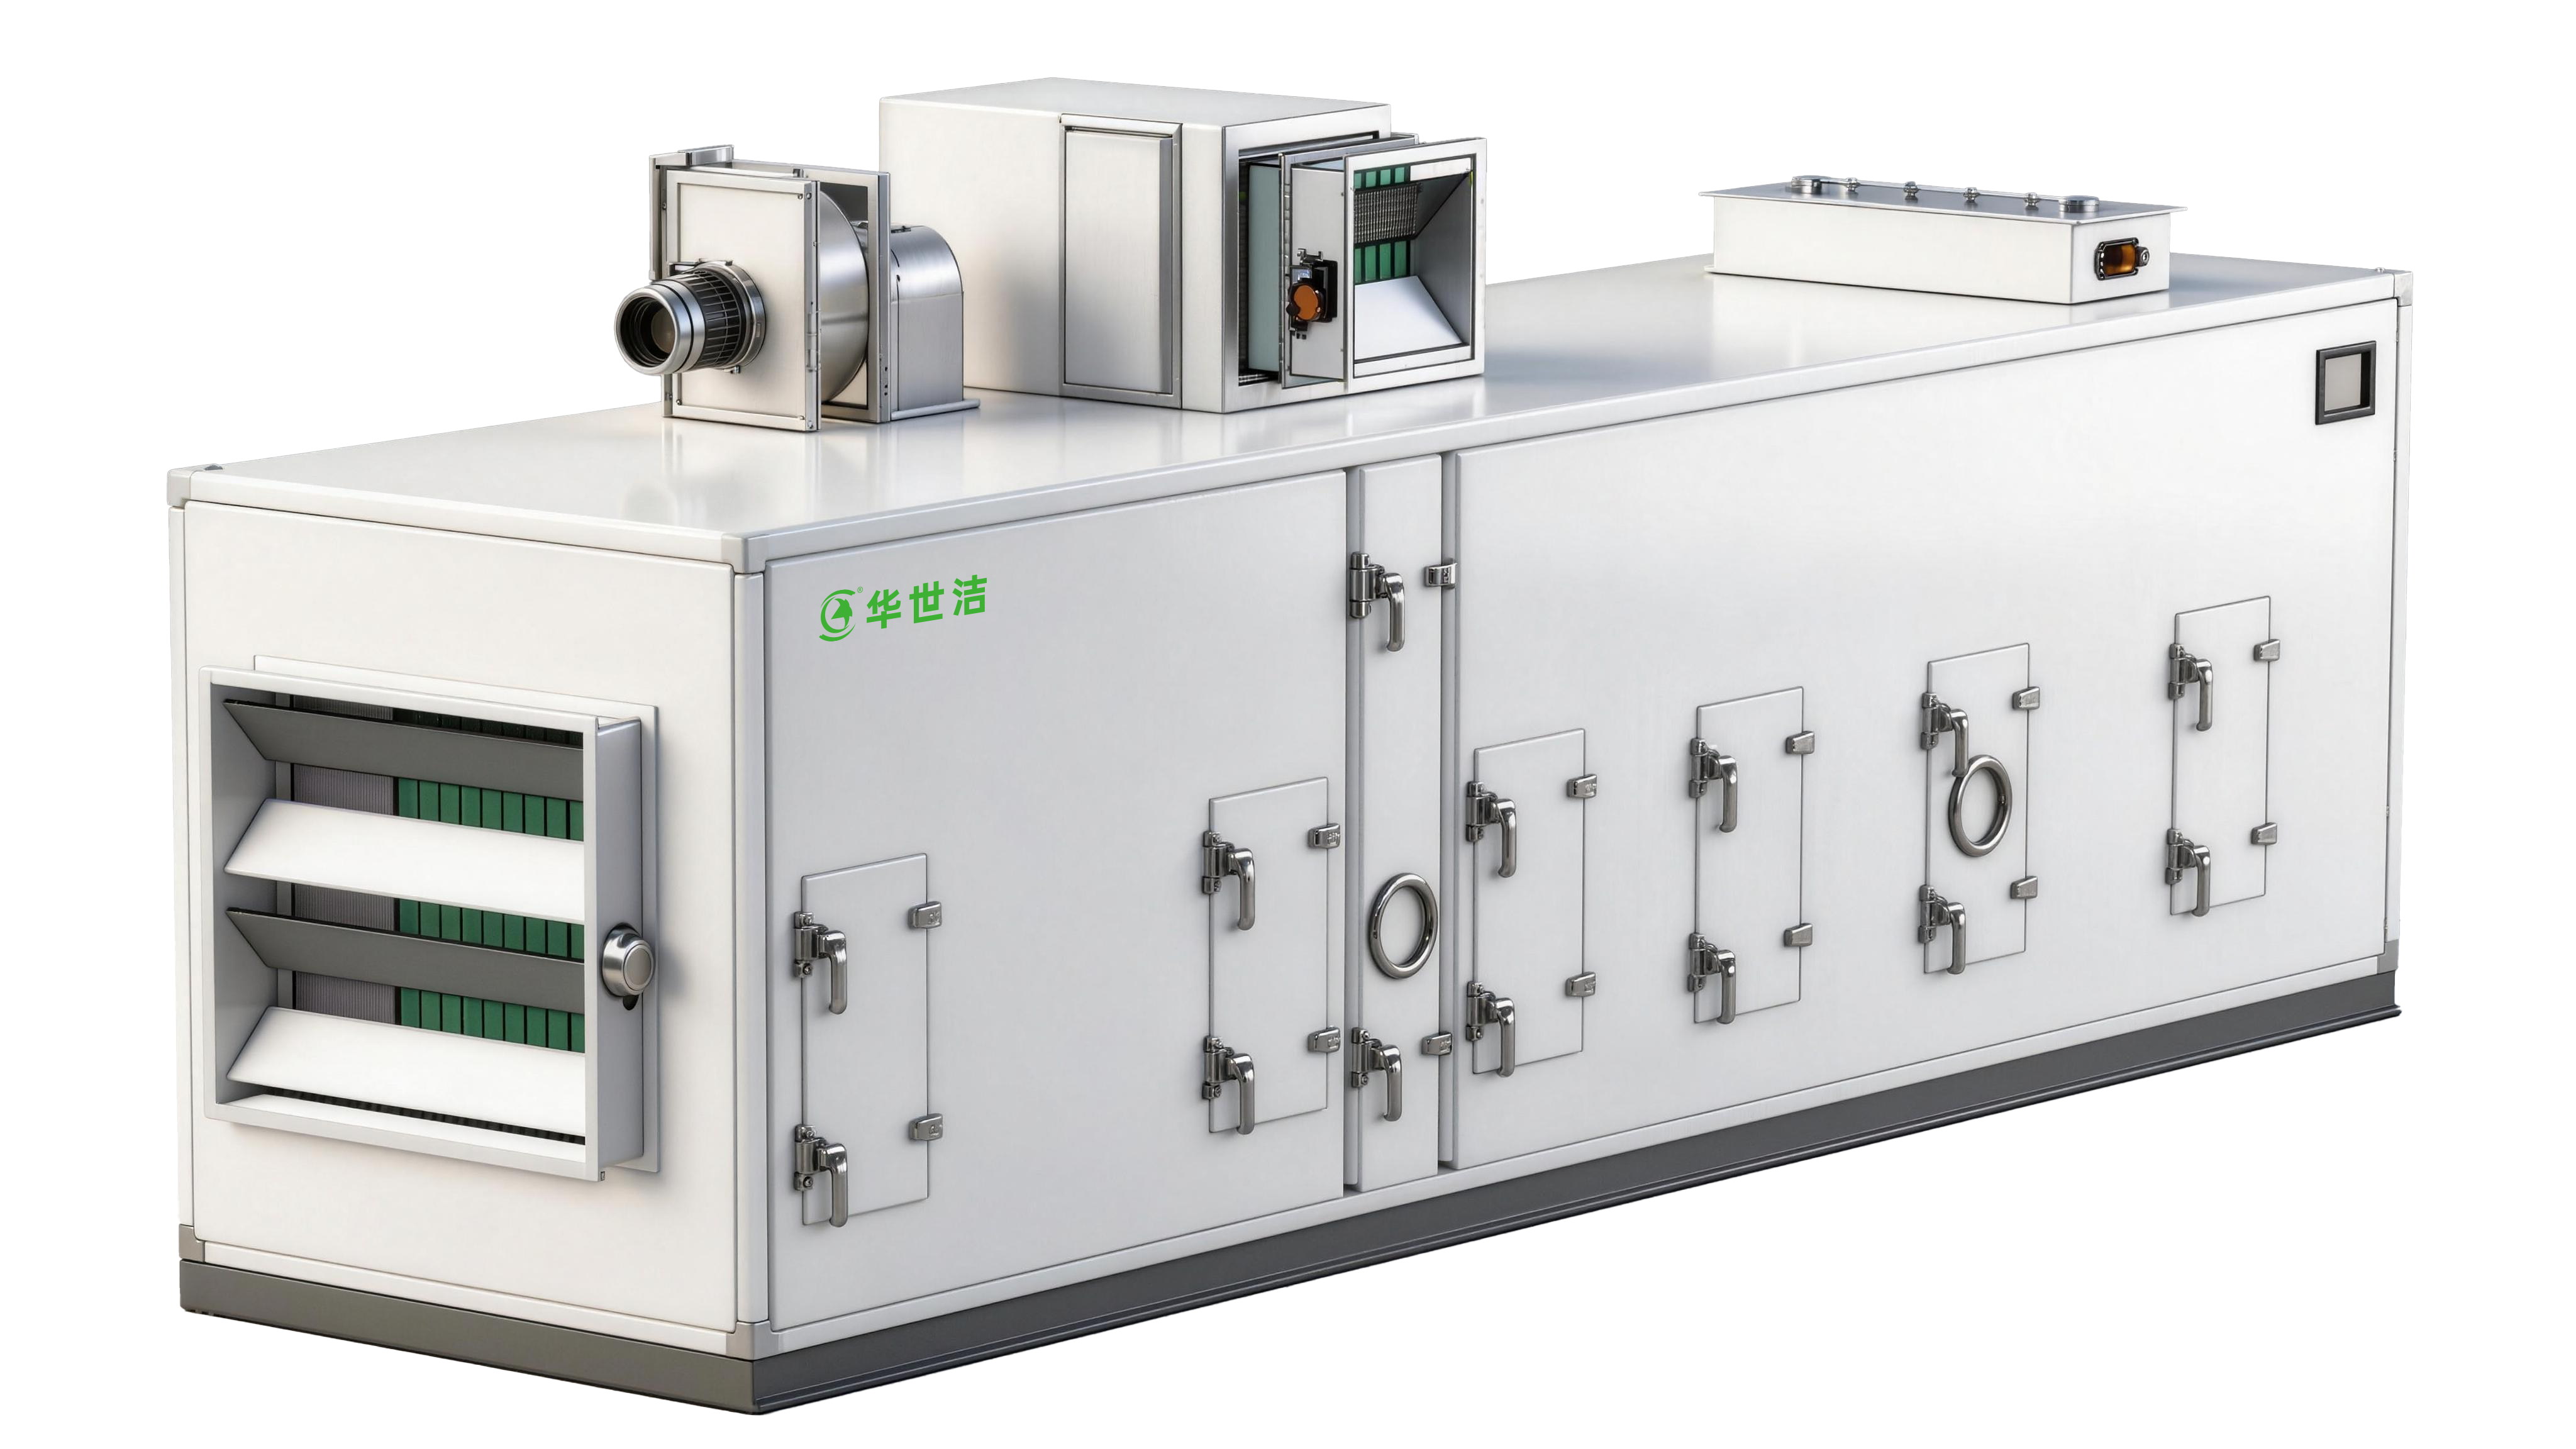
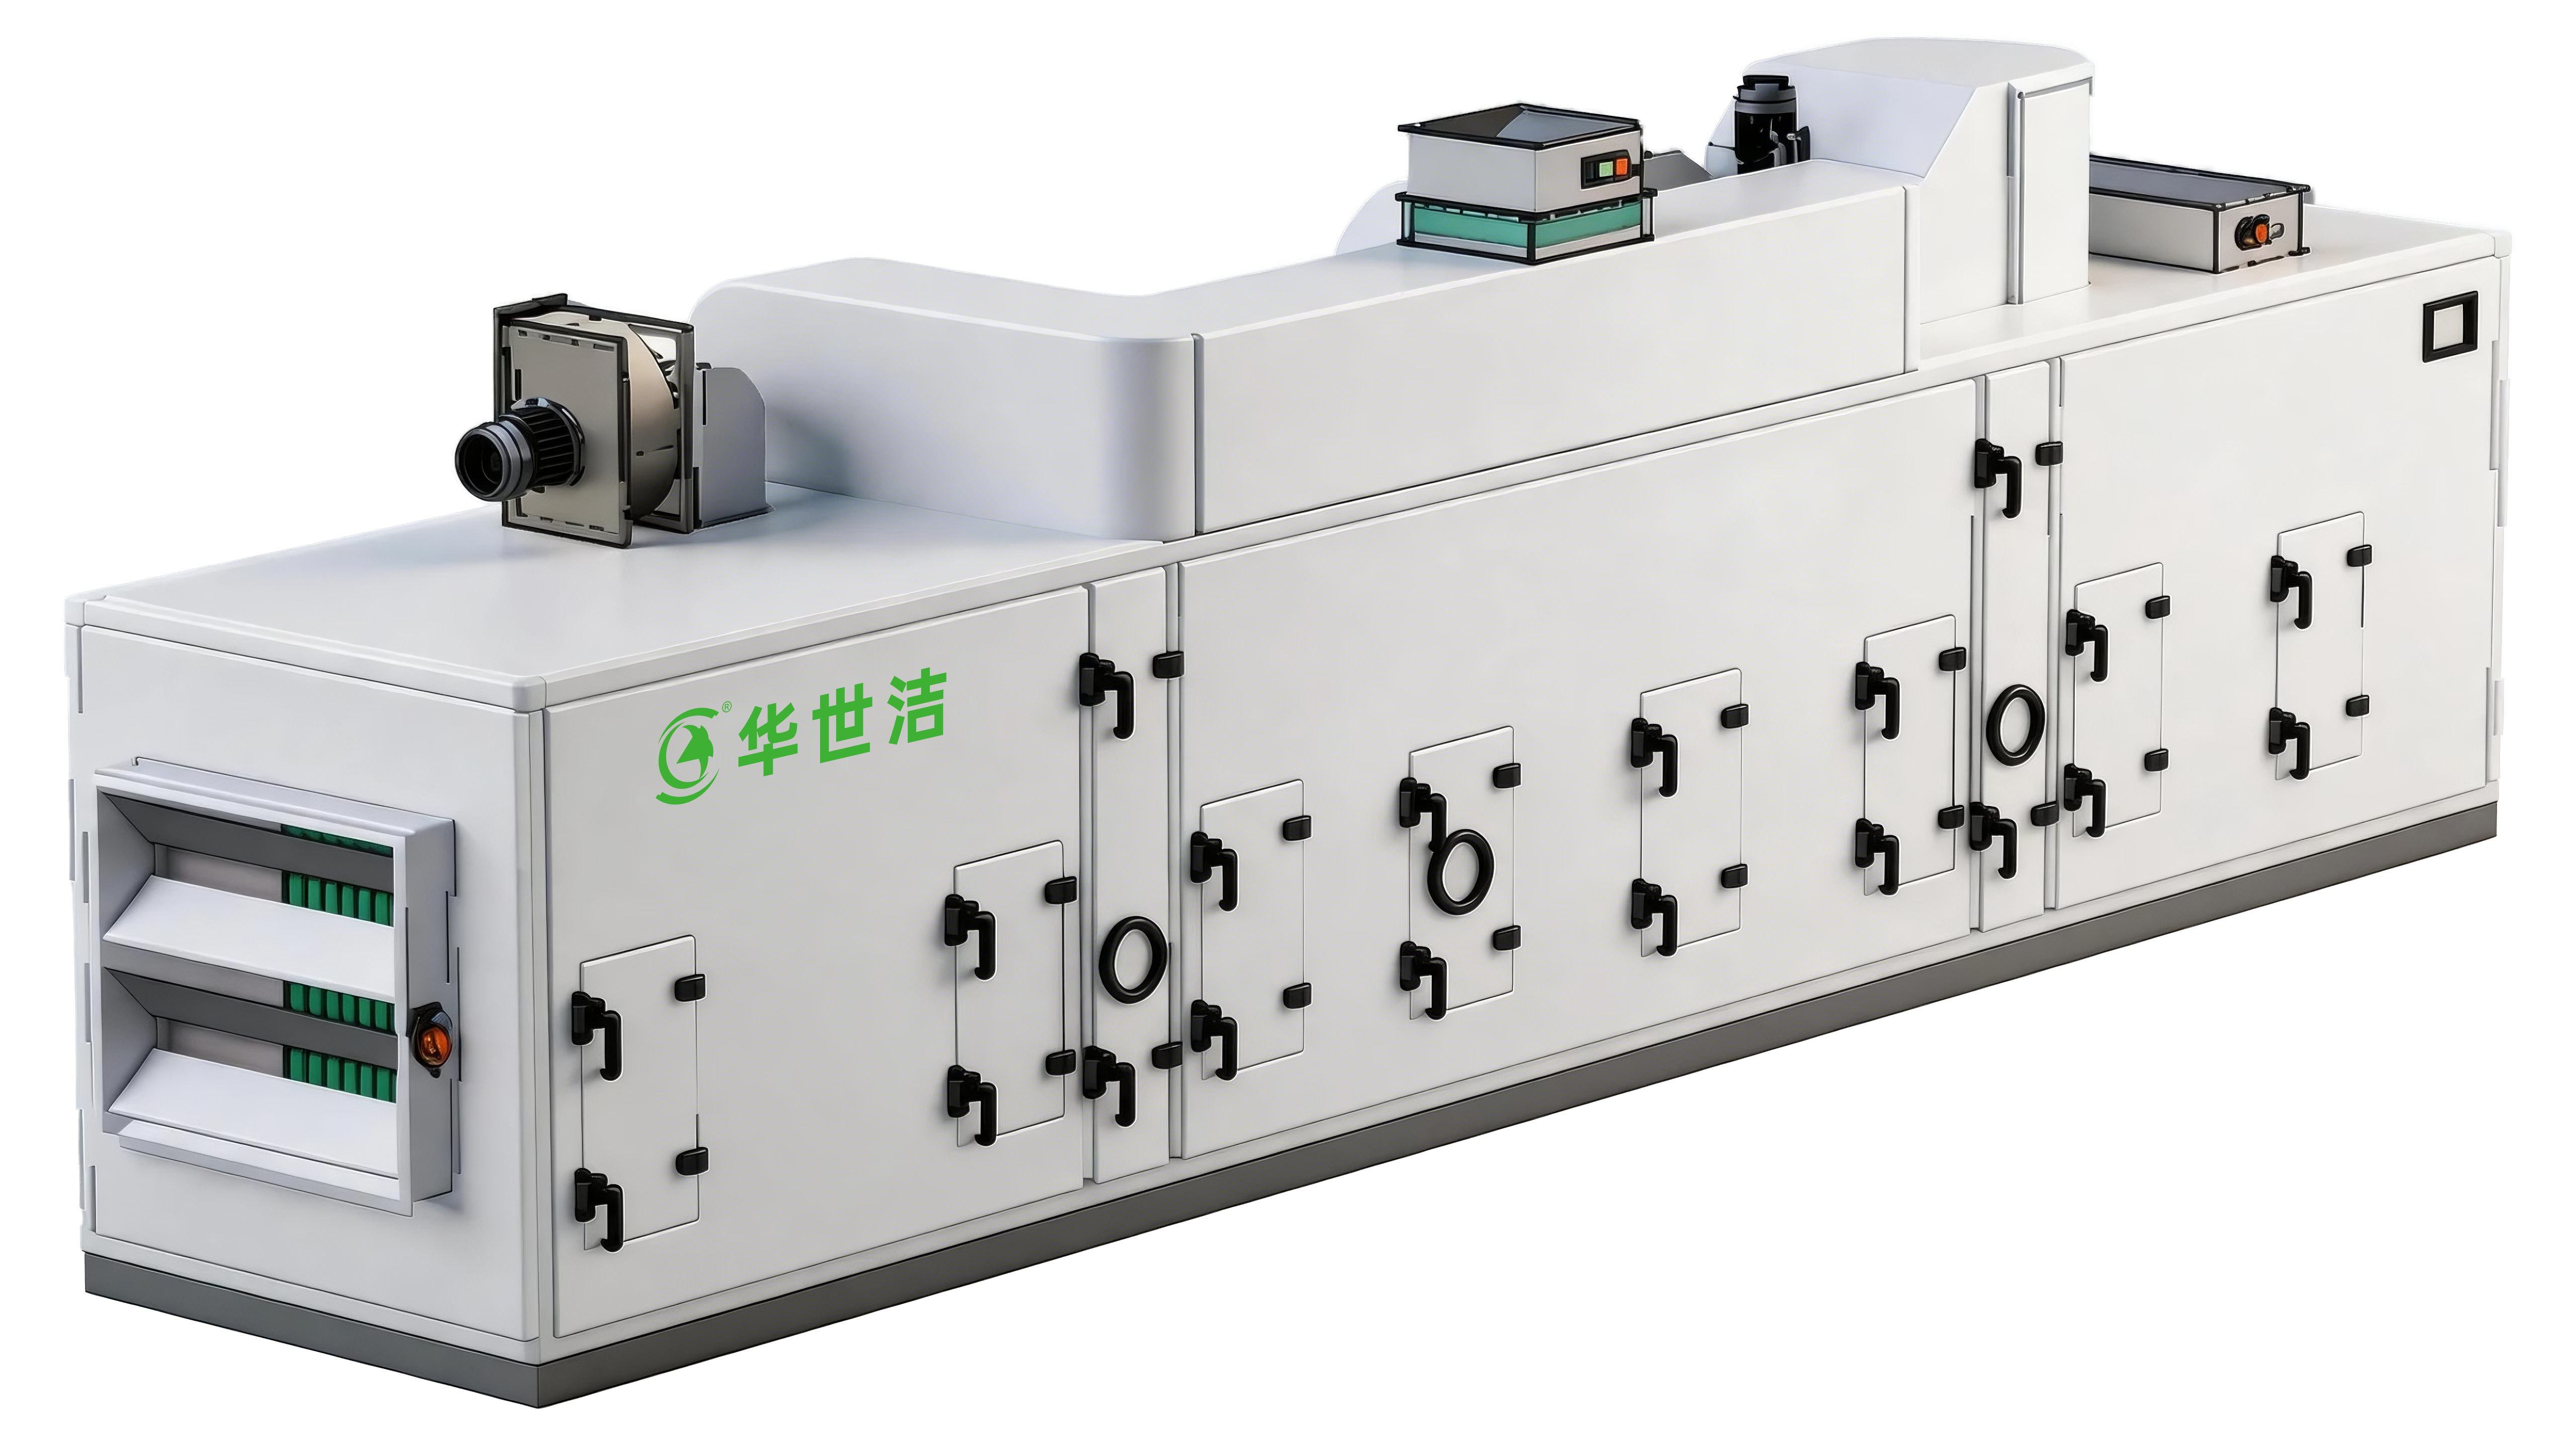
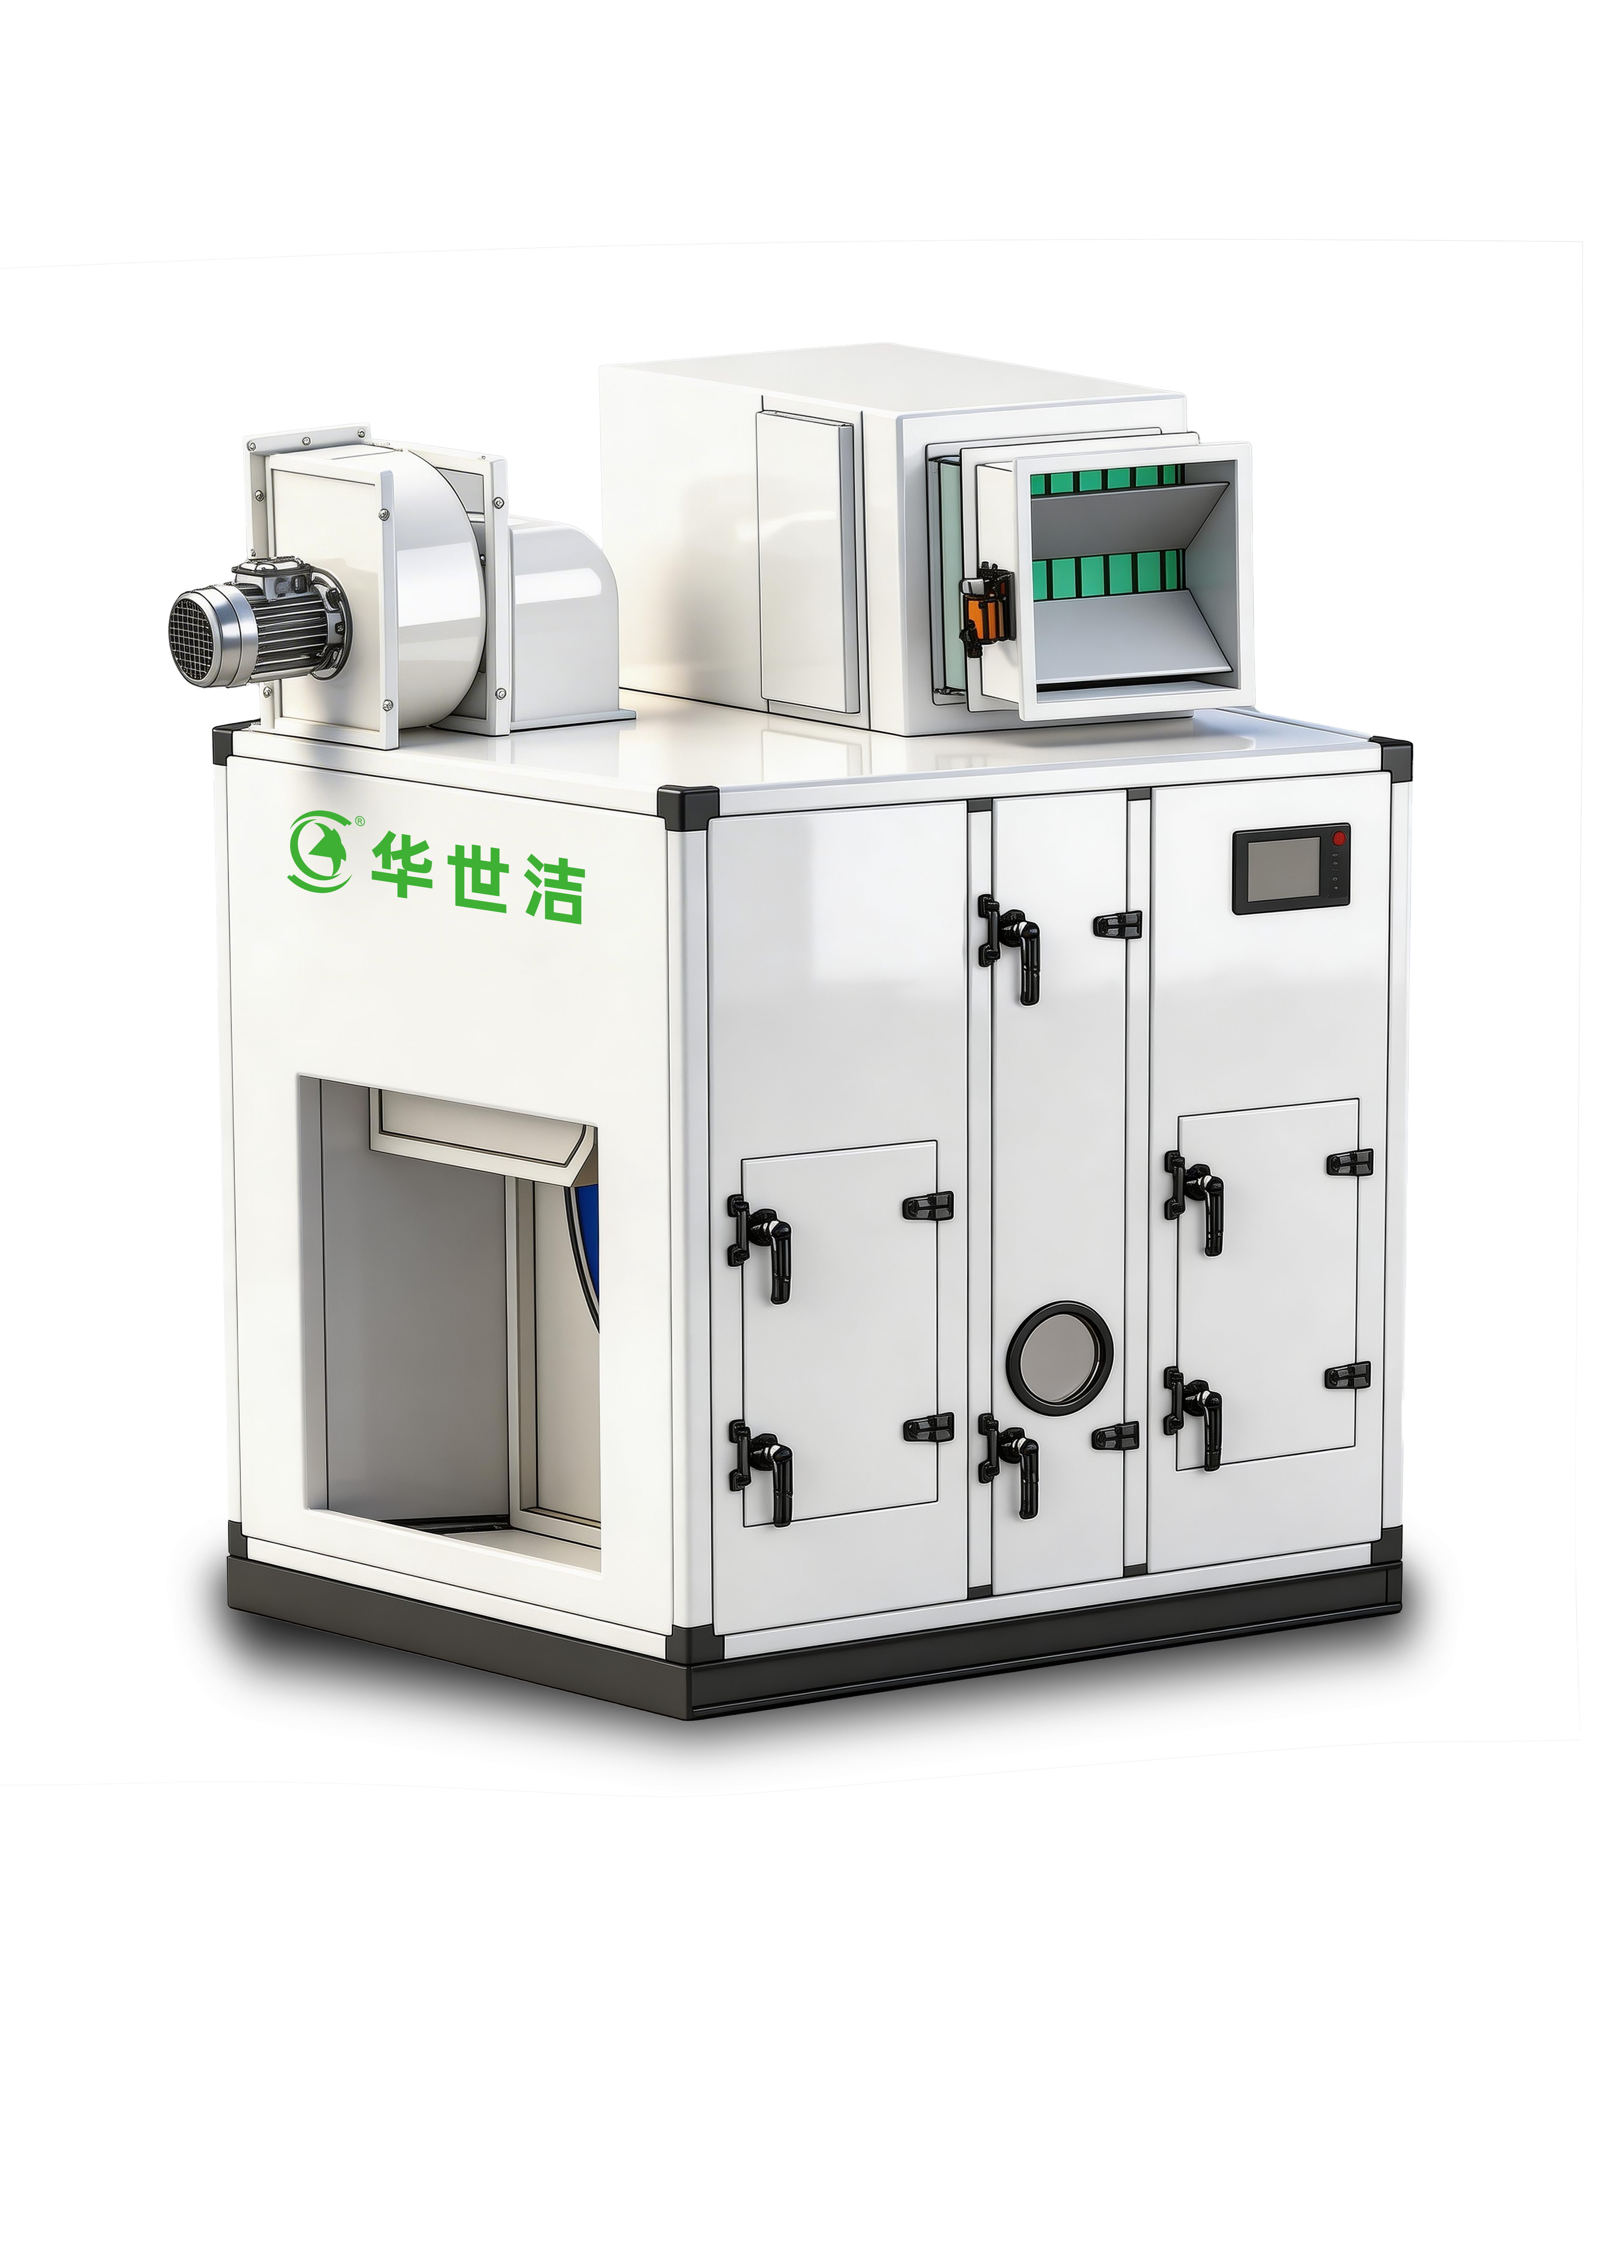
Rotary dehumidifier
Taking advantage of Naboko's own R&D capabilities, the self-developed dehumidification rotor can be applied to scenarios with dehumidification requirements in the lithium battery industry, food industry, pharmaceutical industry, and other fields.
Contact Us400-609-2658
Rotary dehumidifier
Core Advantages
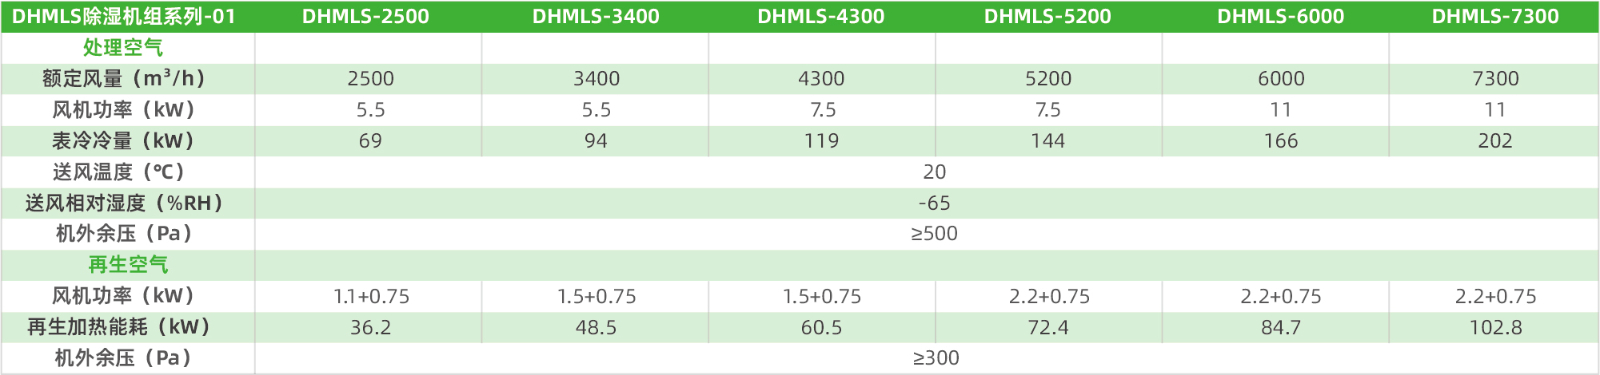
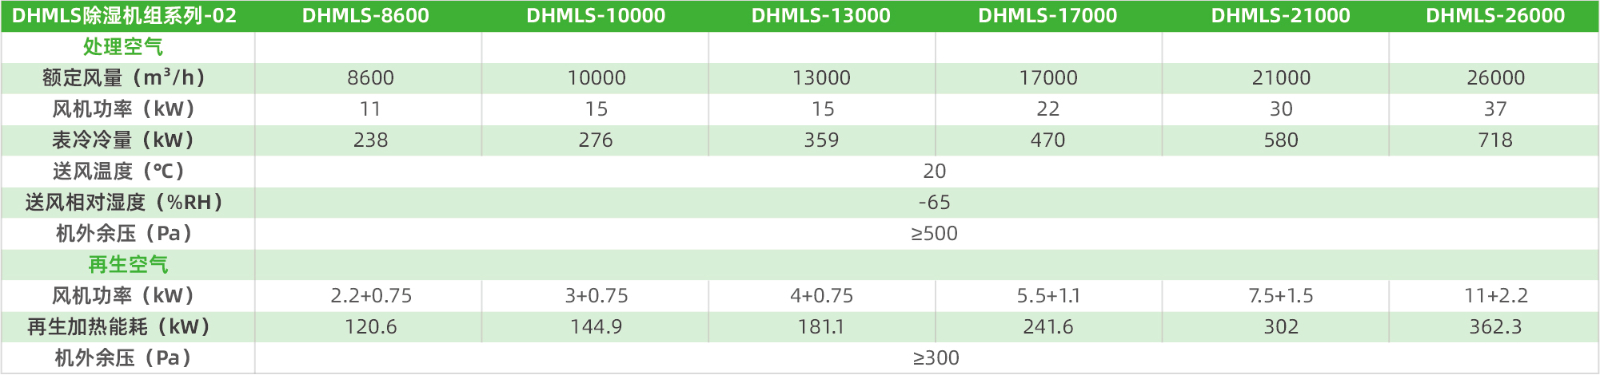
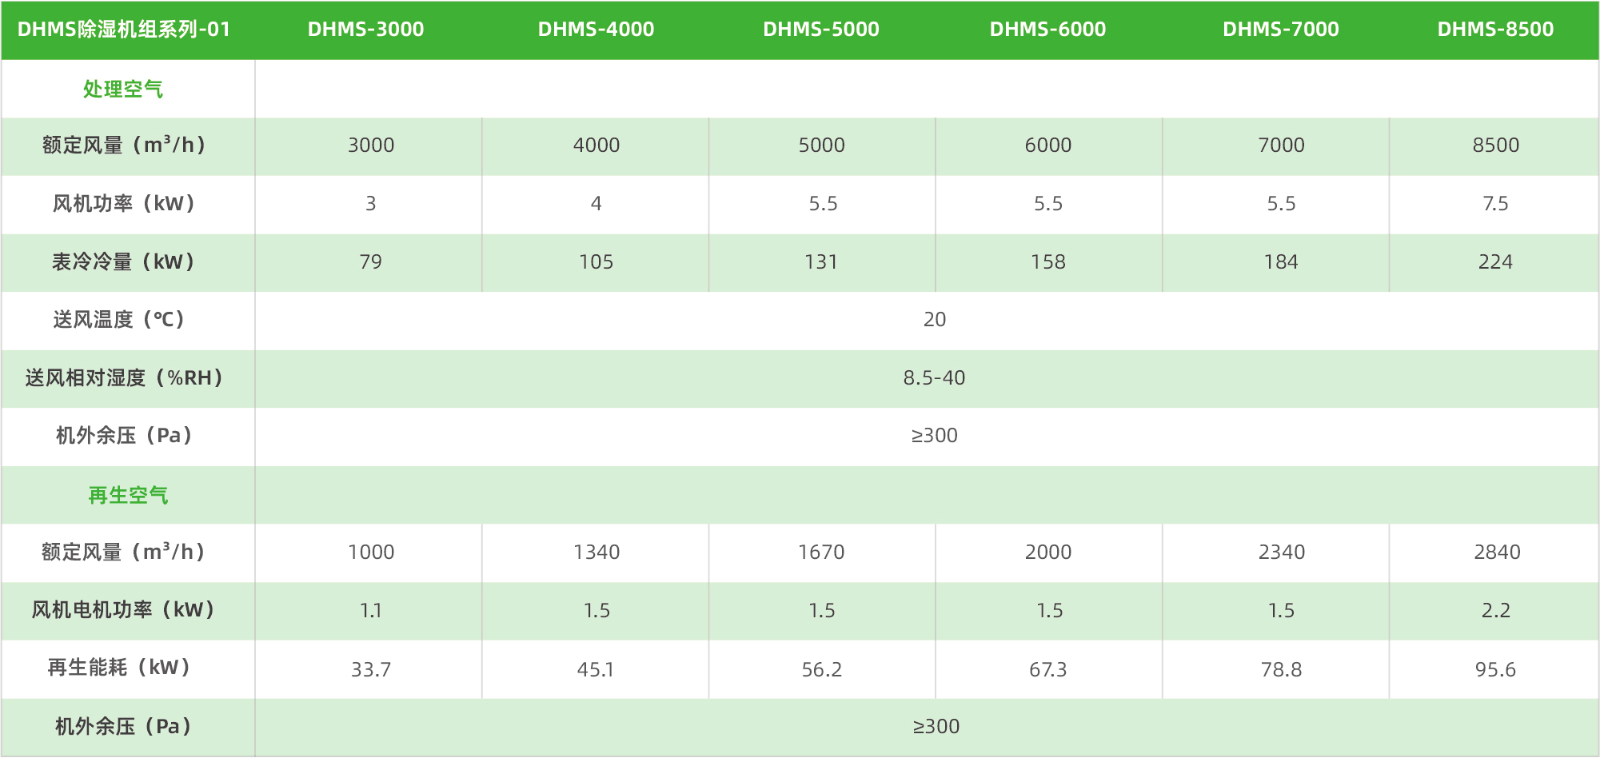
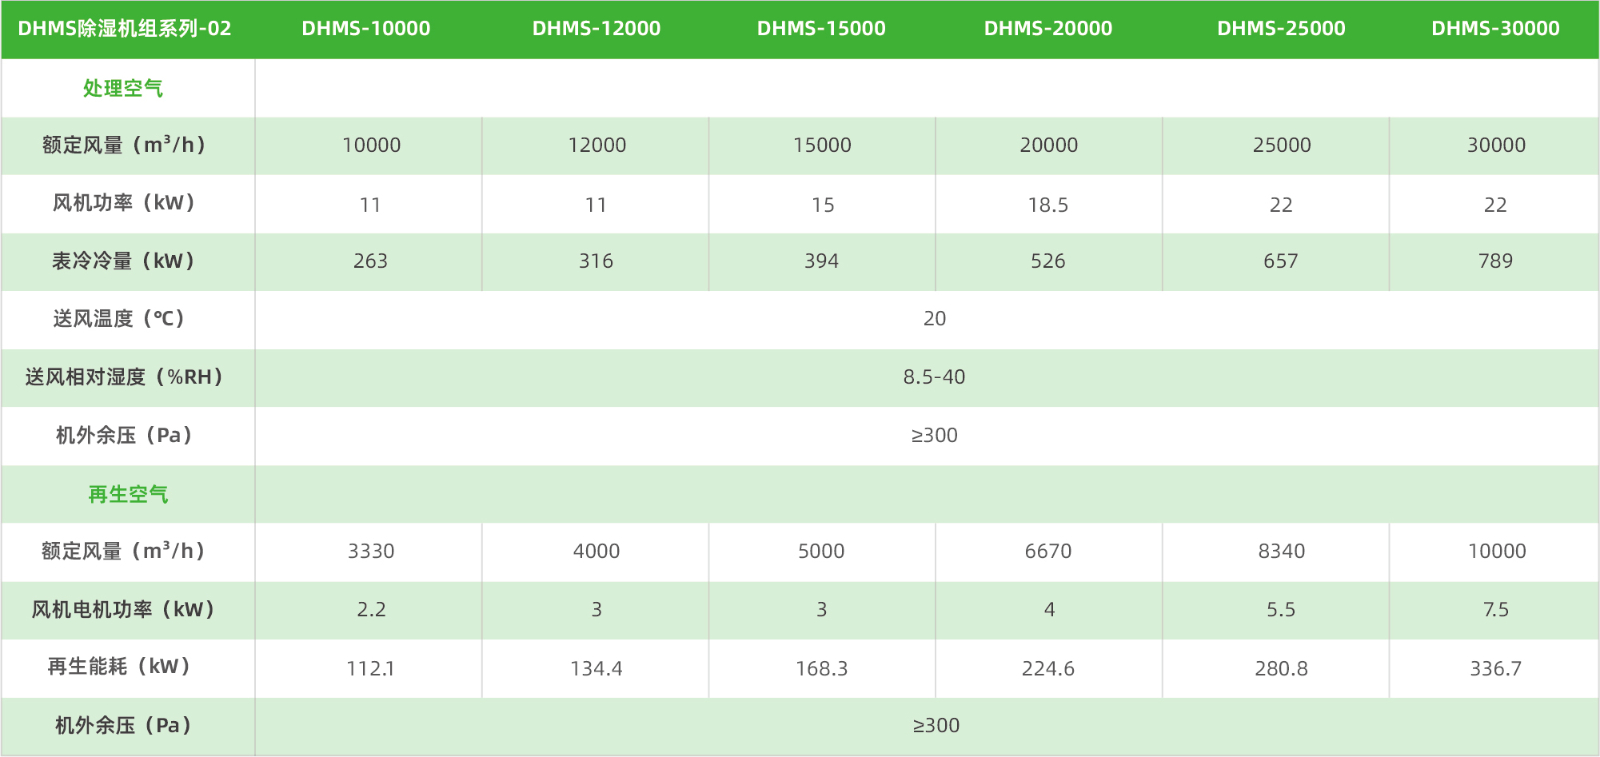
Product Specifications
Ultra-low dew point, extreme dryness
Dual rotor co-operative dehumidification: The primary rotor efficiently pre-dehumidifies, while the secondary rotor deeply adsorbs, reliably achieving an ultra-low dew point of -60℃ to -70℃, with humidity controlled to ≤1%RH
Precise temperature and humidity control: ±0.5℃ temperature control, ±1% RH humidity control, meeting the strict production environment standards of the lithium battery production line.
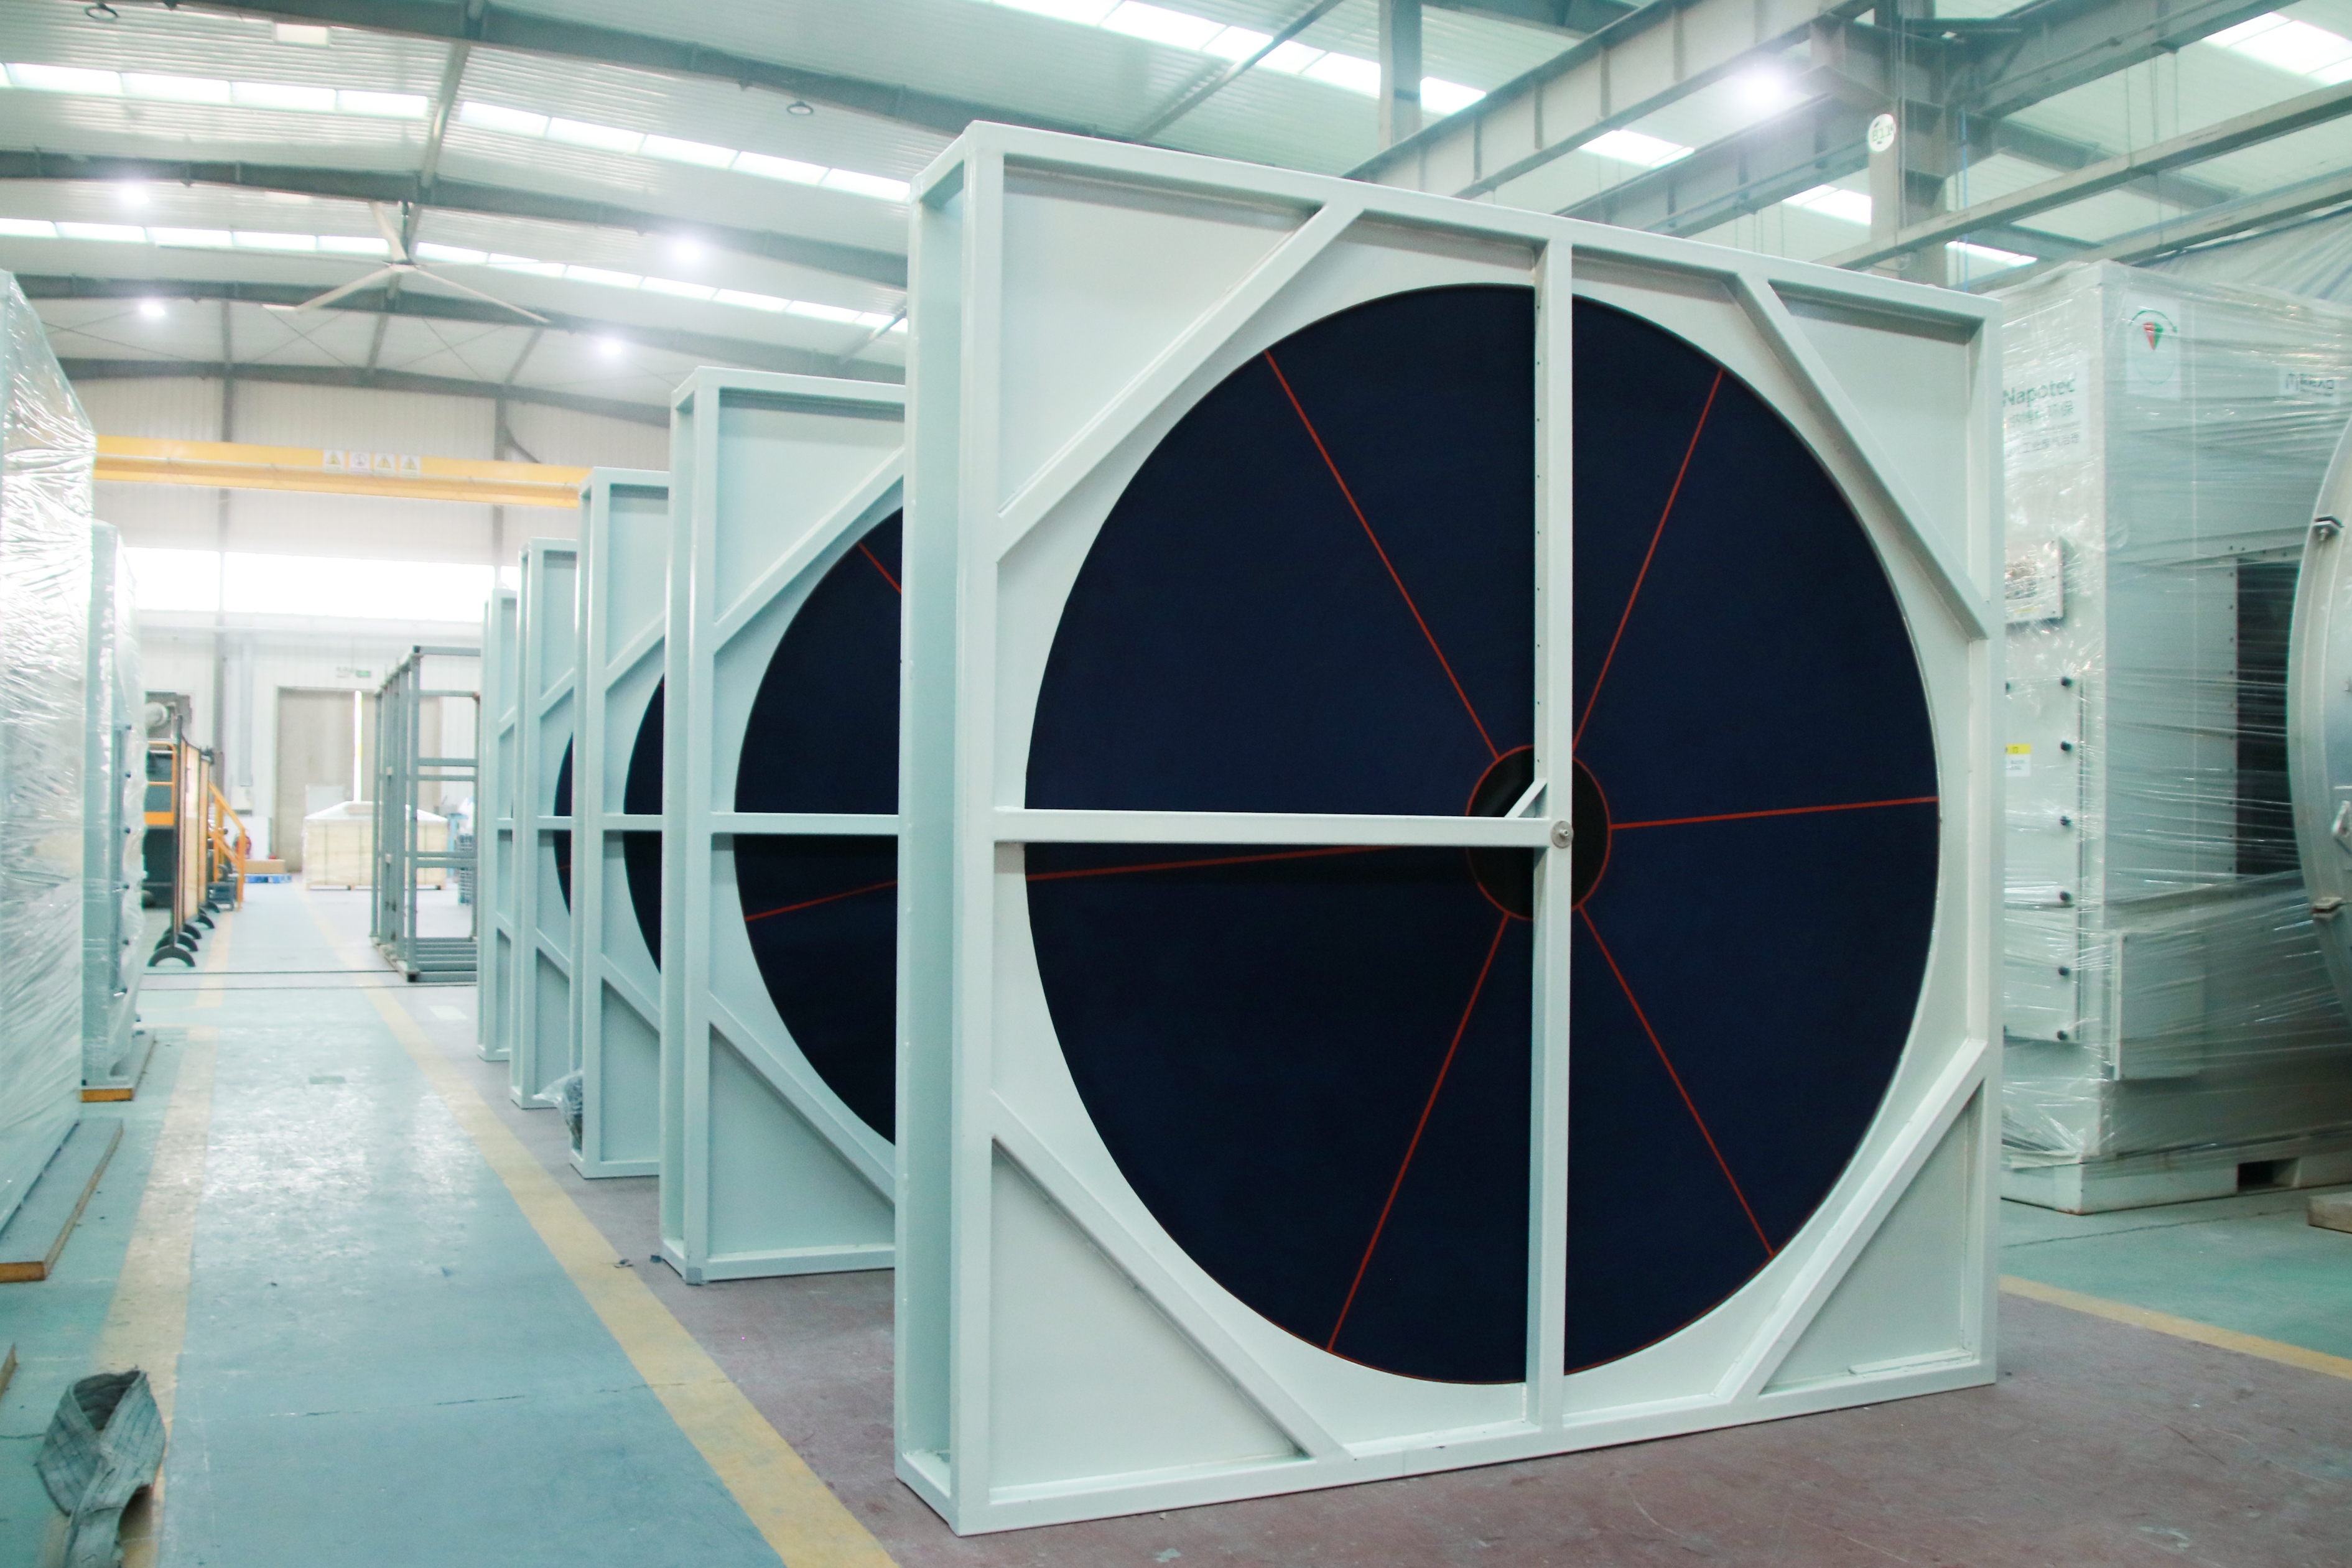
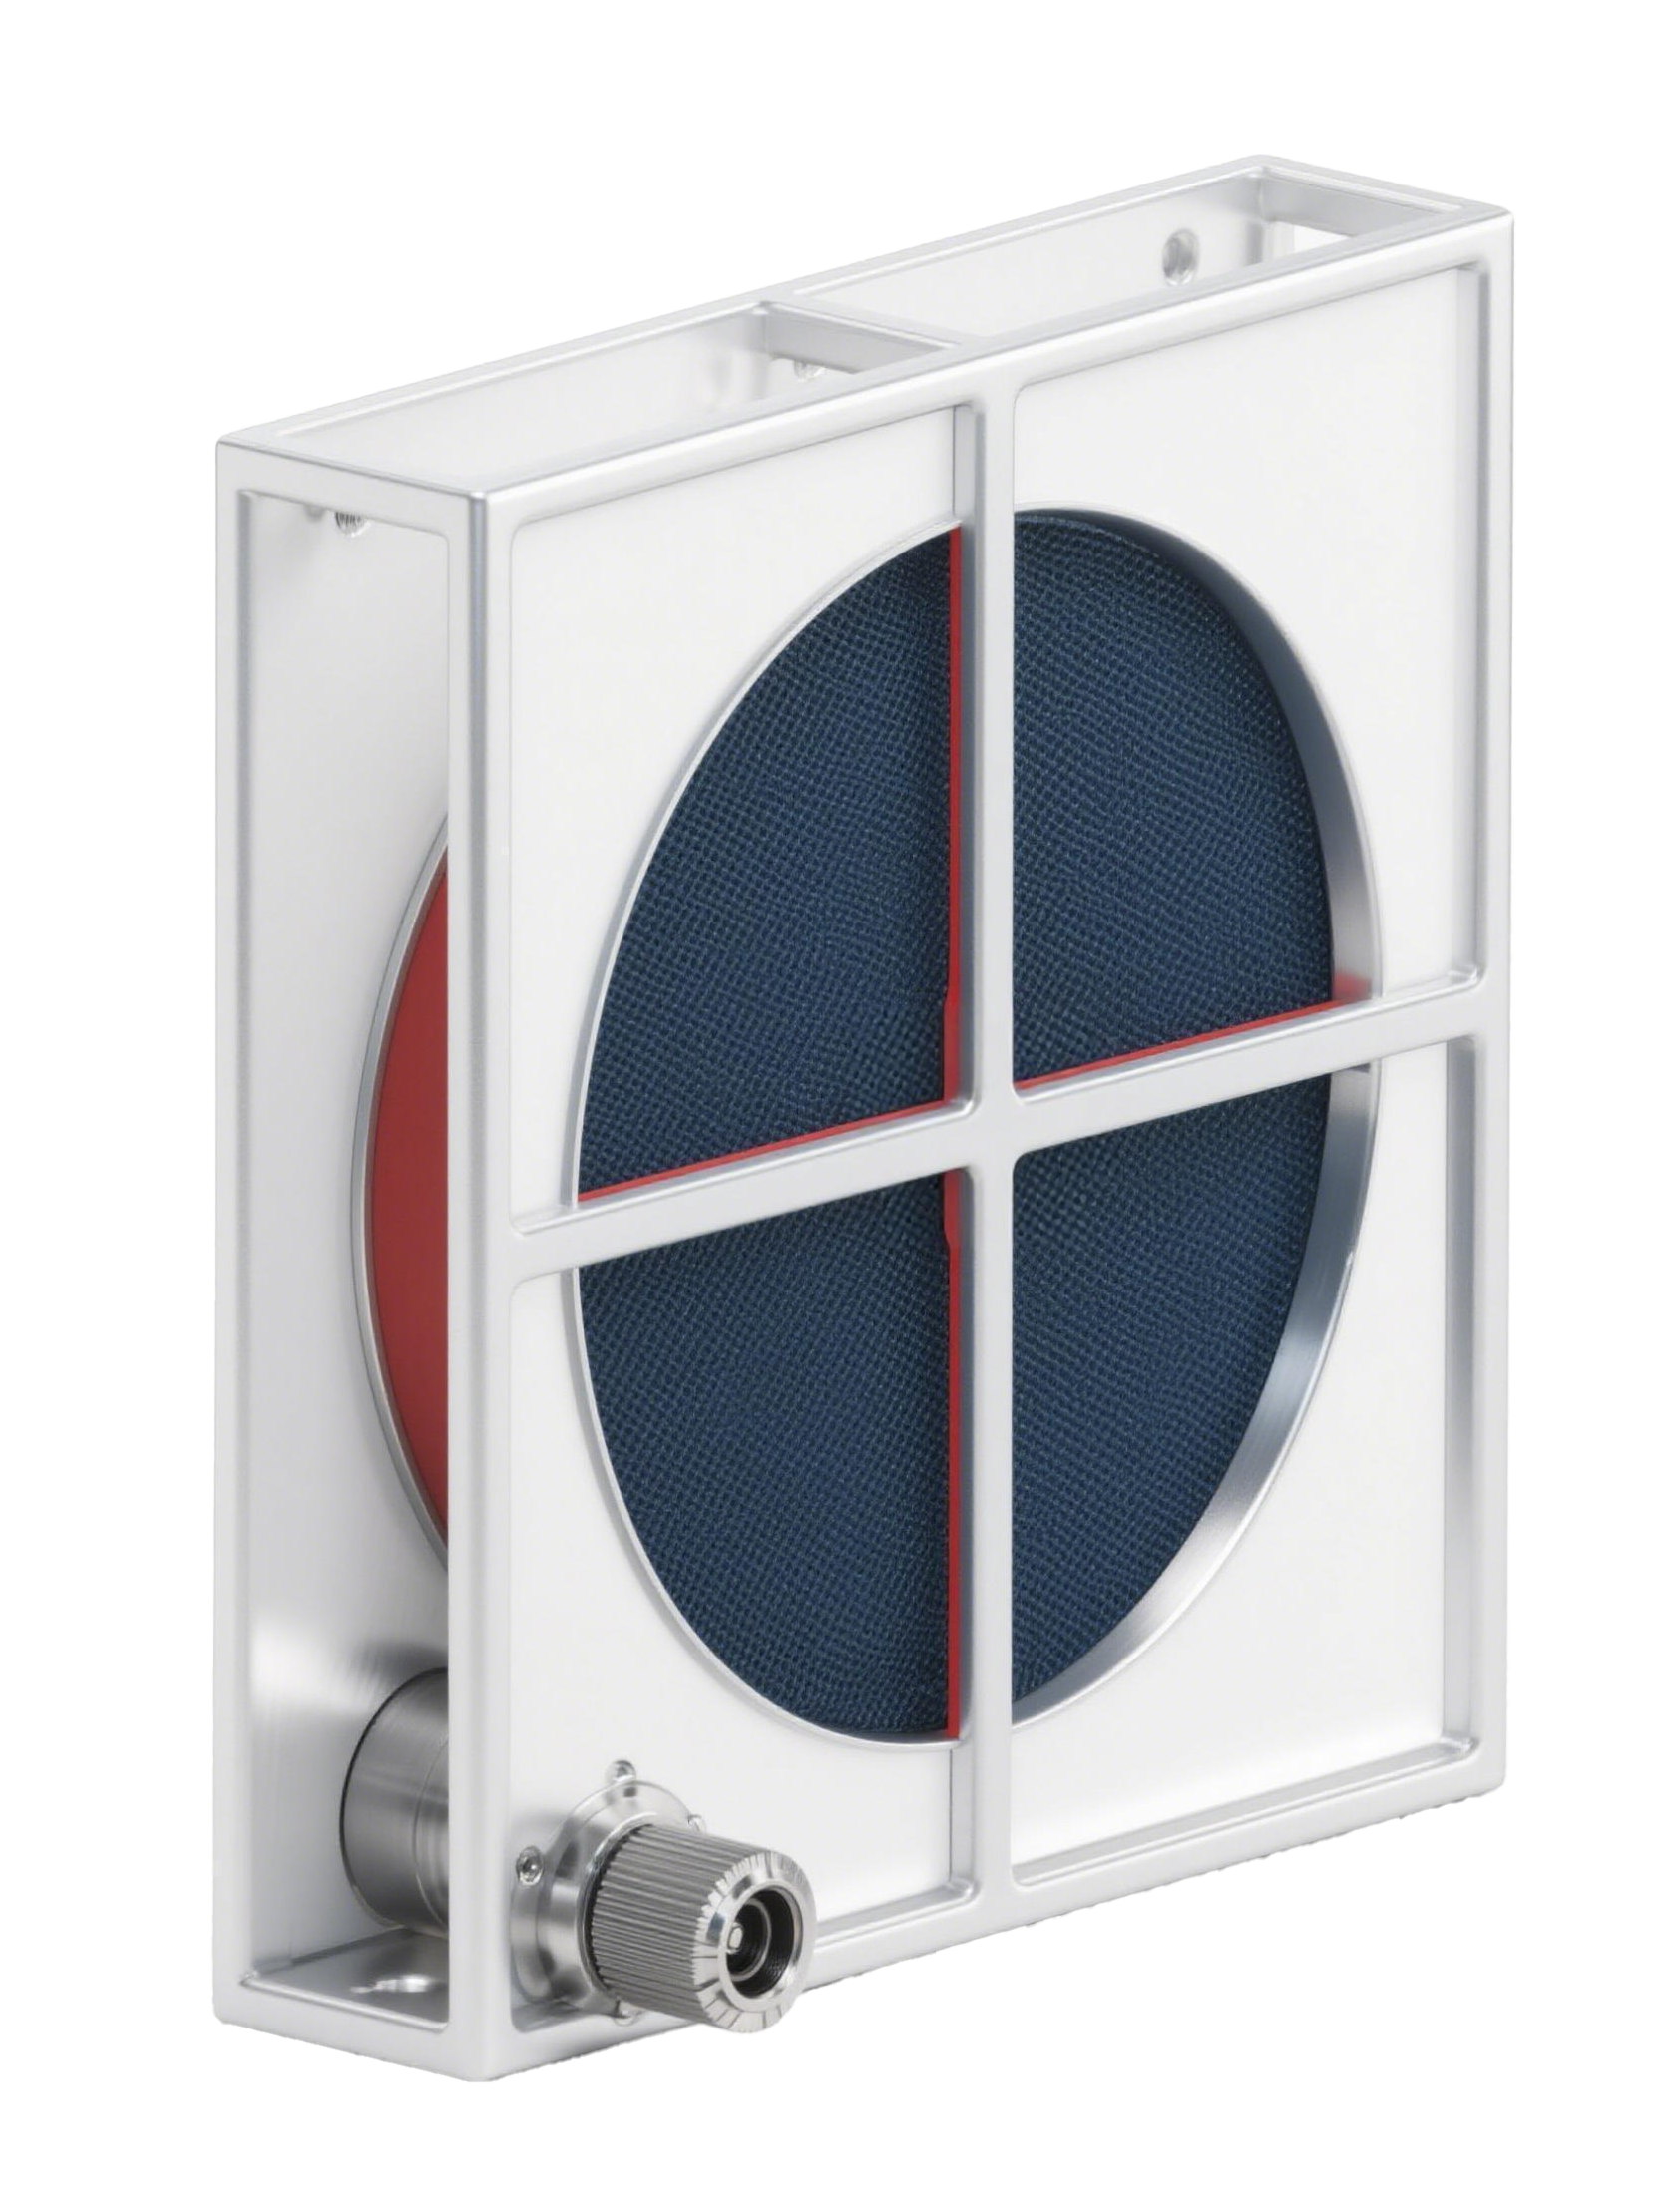
Self-developed high-efficiency dehumidification rotor
Huashi Jie has been deeply engaged in rotor technology for over a decade. They have independently developed four series of dehumidification rotors: modified silica gel, molecular sieve, composite type, and low-temperature regeneration. They possess a unique high-temperature sintering process, zero organic glue molding, A1-level flame retardancy, no odor, no shrinkage, no cracking during long-term operation, and an extended anti-aging life of over 30%. The effective loading capacity of the adsorbent is as high as 78%, enabling deep dehumidification in scenarios with a -78℃ dew point. It has been verified by leading companies in industries such as lithium batteries, food and medicine, and shipbuilding.
Energy conservation and reduction of consumption, cost reduction and efficiency improvement
Reclaimed heat energy recovery: The secondary rotor regenerates air from the high-temperature dry air of the primary rotor, saving 30% to 60% of energy
Heat pump regeneration technology: Suitable for low-grade heat sources of heat pumps, significantly reducing steam/electricity consumption
Variable frequency intelligent regulation: Frequency control for fans/renewal heating, output as needed, operating cost drops by 40%+
Stable and reliable, durable and long-lasting
Self-developed molecular sieve/silica gel composite rotor: Strong adsorption capacity, resistant to pollution, and can operate stably for 24 hours continuously
Modular integrated design: Compact structure, failure rate < 0.3%, easy maintenance, and less downtime
Multiple safety protections: Over-temperature / overload / blockage alarms and interlock protection, ensuring safe operation without worries
Intelligent Control - Convenient Management
PLC + Touch Screen Control System: Real-time monitoring of temperature, humidity, dew point, air volume, and energy consumption
Remote Monitoring + Data Recording: Computer remote operation, fault warning, historical curve export
Automatic Operation Mode: Timed start and stop, humidity linkage, one-click switch, unmanned operation
Related Industry Solutions
Get a Quote
Open Cooperation Channels, Cultivate the Environmental Protection Field Together
Whether you need equipment selection, technical consultation, or win-win cooperation, the Napotec professional team is always at your service.
Document Download
Fill in the information below to download the documents